Choosing a Pipe Swaging Machine is a production decision, not merely a purchase decision. The correct model must match tube material, diameter range, wall thickness, output volume, and required finish. A machine that looks powerful may still create ovality, surface marks, or inconsistent joints.
Industry reports support this cautious approach. Grand View Research identifies automation, precision forming, and energy efficiency as major trends in the global metal forming machine market. The International Federation of Robotics also reports continuing growth in industrial automation, especially where repeatability and labor efficiency matter. These trends affect swaging workshops directly. However, market forecasts are not machine specifications. They cannot replace a sample test with your actual tubing.
Professor Matthias Merklein, a respected metal-forming researcher at Friedrich-Alexander-Universität Erlangen-Nürnberg, has emphasized, “The whole process chain must be considered.” That principle belongs at the center of every buying decision. Consider tooling changes, lubrication, noise, maintenance access, operator training, and after-sales support. Small details matter. A ten-minute setup delay can become hours of lost output each week.
This guide presents seven practical tips for choosing a Pipe Swaging Machine. It examines capacity, control systems, tooling flexibility, safety design, operating costs, and supplier credibility. No checklist is perfect. I have seen buyers focus heavily on rated force and overlook service response time. That shortcut can be expensive. Compare verified test results, request trial samples, and question every impressive specification before signing an order.
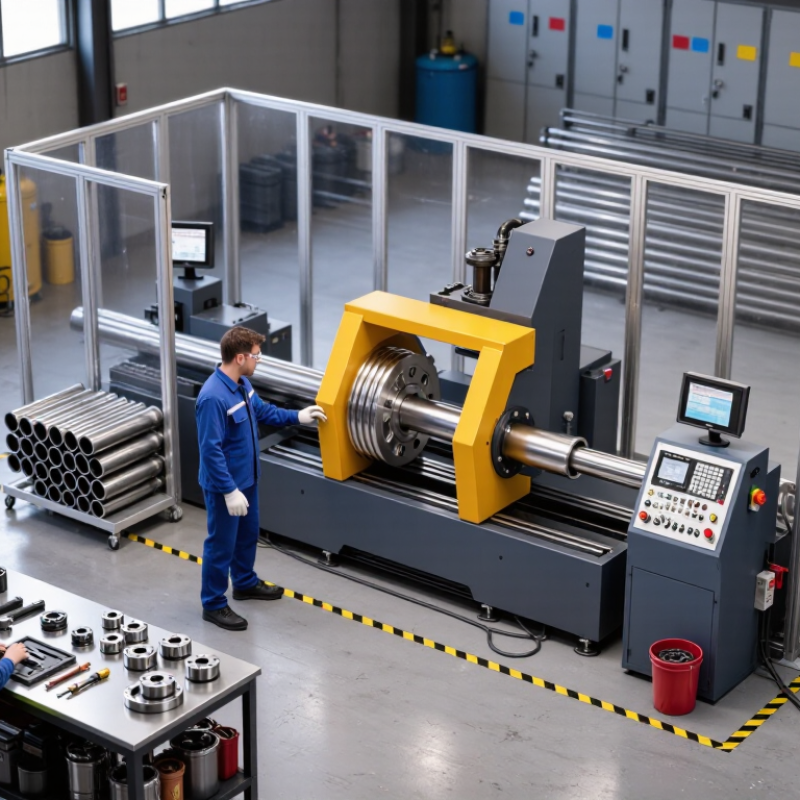
A pipe swaging machine reshapes a pipe end by reducing or forming its diameter through controlled pressure. It usually works with dies that compress the tube evenly around its circumference. That is the core job.
Unlike cutting, swaging changes the metal without removing material. The forming action may be radial, axial, or a combination of both. Die movement, feed speed, lubrication, and material hardness all affect the final shape. Excessive force can create wrinkles, cracks, or uneven wall thickness. Poor alignment may leave the pipe visibly off-center. Small details matter.
When choosing a machine, match its working range to the pipe’s material, outside diameter, wall thickness, and required profile. More capacity is not always better. A machine with excessive force may reduce control on smaller tubes. Check adjustment accuracy, die replacement time, guarding, and emergency controls. These features influence daily reliability, not just purchase cost.
I once underestimated the effect of surface condition during forming. A slightly contaminated pipe caused inconsistent results. That mistake showed me why cleaning and inspection belong in the operating process. Test a sample piece before production, then measure diameter, length, and wall thickness at several points. Review the results against approved drawings and technical requirements. Some machines also need trial adjustments because real material rarely behaves exactly like a catalog example.
The chart shows typical single-pass diameter-reduction ranges used as practical planning references for cold pipe swaging. Actual results depend on material grade, wall thickness, tooling geometry, lubrication, machine force, and workpiece support. When selecting a machine, verify its maximum tube diameter, available forming force, stroke or feed rate, die compatibility, control accuracy, and safety features.
Choosing a Pipe Swaging Machine: Define Required Pipe Sizes, Materials, and Swaging Capacity
Accurate sizing prevents expensive mistakes. Record the smallest and largest outside diameters, wall thicknesses, and finished end dimensions. Include dimensional tolerances. A machine rated for diameter alone may not handle thicker walls or longer reduction zones. Measure actual pipes, not only drawing values.
Material selection matters just as much. Stainless steel, carbon steel, aluminum, and copper respond differently to forming pressure. Harder alloys may require greater force, stronger dies, or several forming passes. Check the material grade, hardness range, and work-hardening behavior. Ask for sample trials using your own pipe. A clean test result is useful, but one successful sample proves little. Repeat it.
Swaging capacity also includes stroke length, maximum reduction, die clearance, and production speed. Confirm whether the machine supports your required tooling and future sizes. Inspect the frame, clamping system, controls, and emergency protections. These details affect repeatability and operator safety. I have seen specifications appear suitable until a real tube exposed vibration or uneven clamping. Leave operating margin rather than choosing the exact limit. It costs more initially, but overloaded equipment can create poor ends, damaged dies, and inconsistent measurements. Check maintenance access, spare tooling availability, and service documentation before purchase. A practical trial sheet should record pipe material, dimensions, force, cycle time, and final tolerance.
| Tip | Specification to Define | Practical Planning Data | Why It Matters |
|---|---|---|---|
| 1. Confirm pipe outside diameter | Minimum and maximum pipe outside diameter (OD) | Example production range: 12–60 mm OD. Common nominal tube sizes in this range include 12, 16, 20, 25, 32, 40, 50, and 60 mm. | The machine tooling, die opening, frame clearance, and forming force must cover the complete OD range without exceeding the rated capacity. |
| 2. Define wall thickness | Minimum, nominal, and maximum wall thickness | A representative light- to medium-wall tube range is 0.8–3.0 mm. The exact limit depends on OD, material strength, die design, and the required reduction or expansion. | Wall thickness affects forming load, risk of buckling, end cracking, and the number of forming stages required. |
| 3. Match the pipe material | Material grade, yield strength, ductility, and surface condition | Typical materials: • Low-carbon steel: approximately 200–350 MPa yield strength • 304 stainless steel: approximately 200–300 MPa yield strength • 6061-T6 aluminum: approximately 240 MPa yield strength | Higher-strength or less-ductile materials generally require greater force, better lubrication, controlled speed, or multiple passes. |
| 4. Calculate swaging capacity | Maximum forming diameter, wall thickness, reduction ratio, and available force | For preliminary selection, specify the largest OD and wall thickness together, not separately. A sample requirement may be 50 mm OD × 2.5 mm wall with a 10–20% end reduction. | A machine rated for a large diameter may not achieve the same capacity at maximum wall thickness or with high-strength alloys. |
| 5. Select the forming method | Rotary, radial, hydraulic, mechanical, or other forming process | Use rotary or radial swaging when gradual circumferential forming and repeatable ends are important; use hydraulic or mechanical systems when a defined axial stroke and high production force are required. | The process determines tooling flexibility, noise, cycle behavior, end geometry, and suitability for thin-wall or hard materials. |
| 6. Check production requirements | Cycle time, daily output, setup time, and automation level | For planning, compare the required output with the complete cycle: loading, clamping, swaging, unloading, inspection, and die change. A 30-second forming stroke does not necessarily mean a 30-second finished-part cycle. | Actual throughput is controlled by handling and setup time as well as the forming stroke. |
| 7. Verify tooling and quality controls | Die availability, dimensional tolerance, concentricity, surface finish, and inspection method | Define the finished-end dimensions, allowable ovality, transition length, surface marks, and inspection tools such as plug gauges, calipers, micrometers, or coordinate measurement equipment. | Correct tooling and measurable acceptance criteria are essential for consistent fit-up, sealing, welding, and assembly. |
Choosing a pipe swaging machine starts with the forming method, not the brochure’s maximum force. Rotary swaging suits repeated diameter reduction and thin-wall tubes. Hydraulic press swaging handles heavier sections and controlled axial forming. Mechanical machines can deliver fast cycles, but adjustment may feel less forgiving. More tonnage? Not always. Excessive force can mark the tube, increase tool wear, and waste energy.
Match the machine type to your material range. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023. That scale reflects broad material variation, including carbon steel, stainless steel, and alloy grades. Ask for verified trials using your actual tube diameter, wall thickness, hardness, and target reduction. Check ovality, surface marks, end length, and tool life after several cycles. One successful sample proves very little.
Production flexibility matters when orders change weekly. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturing leaders viewed smart manufacturing as important for competitiveness. Look for quick die changes, programmable recipes, accessible tooling, and useful process records. A CNC-controlled machine may reduce setup errors, yet it still needs skilled operators and disciplined maintenance. I would compare changeover minutes, not only hourly output. A machine that runs quickly but sits idle during tooling changes may be the weaker investment. This is easy to overlook.
Accuracy starts with the finished tube, not the machine brochure. Ask for repeatability data, stroke control, and documented test methods. ISO 230-2:2014 provides a useful framework for checking positioning accuracy. Measure several swaged parts at operating temperature. Cold trials can hide drift. My own caution: impressive first-piece results may not represent an eight-hour production run.
Safety deserves equal attention. Confirm guarding around the die, emergency stops, two-hand controls, and safe access during tooling changes. OSHA 1910.212 requires protection from machine hazards at the point of operation. The U.S. Bureau of Labor Statistics recorded 5,283 fatal work injuries in 2023. That figure is not swaging-specific, but it reinforces a practical lesson: safety features must be usable, not decorative.
Maintenance affects accuracy and ownership cost. Review lubrication points, hydraulic inspection steps, spare-part access, and fault diagnostics. A maintenance log should show service intervals in hours, not vague promises. Check whether dies, mandrels, adapters, and tube supports match your actual sizes. Tooling that requires improvised adjustments creates inconsistent results. Also ask about changeover time. A machine may be precise, yet inefficient when every diameter needs a different setup. Leave room for honest doubt: supplier specifications rarely describe dust, operator variation, or worn tooling. Trial the machine with representative material before purchase.
Choosing a pipe swaging machine requires more than comparing purchase prices. Calculate total cost across five years. Include tooling, dies, installation, training, energy, lubrication, maintenance, and rejected pipes. A cheaper machine may need frequent die replacement. That difference quietly erodes savings.
The U.S. Department of Energy’s Operations & Maintenance Best Practices Guide reports that predictive maintenance can reduce costs by 8–12% compared with preventive maintenance. It may also reduce reactive maintenance costs by 30–40%. Ask whether the supplier provides inspection schedules, spare-parts availability, and service response times. Request realistic cycle-time data for your pipe material and wall thickness. Ask for sample trials. Marketing figures often assume ideal conditions.
Supplier support affects long-term value. Deloitte’s 2023 Global Smart Manufacturing Survey found that 86% of manufacturing executives considered smart manufacturing important for competitiveness. Even a semi-automated swaging machine benefits from clear diagnostics, operator training, and upgradeable controls. Check documentation quality. Check remote support limits. Check local technician coverage. A practical evaluation should include three references using similar pipe sizes. One uncomfortable truth: return-on-investment calculations are rarely perfect. Downtime, operator turnover, and changing orders can distort them. I would challenge my own estimate with a pessimistic scenario, including one week of unexpected stoppage. Reliable value is not the lowest quotation. It is predictable production, maintainable tooling, and support that remains useful after installation.
An exceptional record of quality and service for 35+ years.
© 2026 Excell Battery Co. All rights reserved.Privacy Statement